1. Reduce production costs (core benefit)
1. Reduce new cleaning agent procurement: With a distillation recovery rate of 82%–94%, clean regenerated solvent is directly returned to the cleaning machine for recycling, reducing new solvent procurement by 75%–90%. Hardware terminals are mostly cleaned in large batches continuously, resulting in high solvent consumption and significant cost reduction effects.
2. Significant reduction in hazardous waste disposal costs: Used cleaning agents are classified as hazardous waste, and outsourcing disposal involves high unit costs. After recycling, only small amounts of oil sludge and metal residues remain as hazardous waste, reducing the volume by over 90%. This leads to a notable decrease in hazardous waste transportation frequency and disposal expenses.
3. Fast payback period: Small and medium-sized terminal factories typically recoup their investment within 7-12 months, while enterprises with high production volumes and daily solvent consumption can recover equipment costs in just 4-7 months.
4. Reduce chemical inventory backlog: Avoid bulk stockpiling cleaning agents by relying on solvent recycling to maintain production, thereby freeing up working capital.
2. Stabilize Cleaning Quality and Improve Terminal Yield Rate
Distillation can completely separate stretching oil, stamping oil, rust preventive oil, metal fine powder, and polishing wax, resulting in regenerated solvents with high cleanliness and cleaning power approaching that of new solvents.
2. Avoid solvent aging and emulsification causing oil residue, water marks, white spots, and discoloration on terminal surfaces; prevent defects such as blistering, plating detachment, and poor adhesion in subsequent electroplating, gold plating, and nickel plating processes, thereby reducing rework and scrap.
3. It is compatible with ultrasonic cleaning, spray cleaning, drum cleaning, and fixture tray cleaning, featuring a closed-loop solvent circulation system for the entire workshop, ensuring better consistency in cleaning processes.
III. Environmental Compliance, Effortlessly Handling Environmental Assessments and Factory Inspections
1. Waste organic solvents are classified as hazardous waste and must not be discharged or dumped directly. The equipment achieves on-site waste liquid reduction, meeting clean production requirements, ensuring smooth passage of environmental inspections and impact assessments.
2. The entire sealed recycling system reduces solvent evaporation, lowers VOC emissions in the workshop, improves the working environment for operators, and serves as a key advantage in audits for downstream connector major clients under IATF16949, ESG, and green factory certifications.
4. Enhance workshop safety production standards
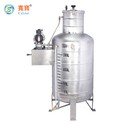
Select an explosion-proof solvent recovery machine with fully enclosed distillation and condensation to minimize the accumulation of waste liquid drums and new solvent drums in the cleaning workshop, thereby reducing the risks of flammable solvent leaks and fire hazards.
The solvent undergoes internal circulation and regeneration, reducing reliance on externally purchased cleaning agents and preventing delays in terminal production line deliveries due to market shortages or price increases.